 |
|
|
|
Certification

- I'm Online Chat Now
Low Noise Level Chain Mesh Conveyor Belt Capable of Speed 50 Feet Per Minute Providing Performance in Harsh Environments

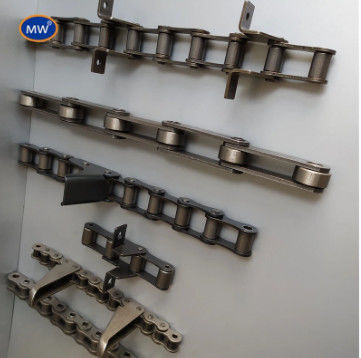
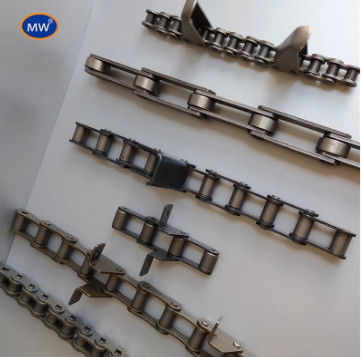
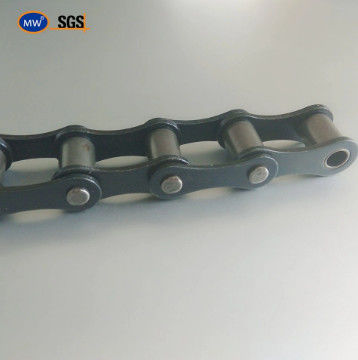
Detailed Product Description
| Temperature Range: | 0-300 Degrees Fahrenheit | Width: | 2 Inches |
|---|---|---|---|
| Standard: | ISO | Booth: | PP/PVC |
| Type: | Conveyor Chain | Speed: | 50 Feet Per Minute |
| Length: | 10 Feet | Powder Recovery Rate: | 99.4% |
Product Description:
The Conveyor Chains are an essential component designed to optimize the performance and efficiency of various industrial conveyor systems. Engineered specifically for applications requiring reliable and consistent material handling, these conveyor chains offer exceptional durability, precision, and smooth operation. With a speed capacity of up to 50 feet per minute, they provide an ideal solution for medium-speed conveyor operations, ensuring a steady and efficient flow of materials through the production line.
One of the standout features of these Conveyor Chains is their compatibility with a wide range of conveyor types, including Grain Chain Conveyor systems, Conveyor Stackers, and Chain Mesh Conveyor Belt setups. This versatility makes them highly valuable in industries such as agriculture, manufacturing, packaging, and logistics, where efficient transportation and stacking of bulk materials are critical. The Grain Chain Conveyor, in particular, benefits greatly from these chains due to their robust construction and ability to handle heavy loads with minimal wear and tear.
The Conveyor Chains are designed with a focus on maintaining a low noise level during operation. This attribute is particularly important in environments where noise reduction is essential for worker comfort and compliance with occupational safety standards. By minimizing operational noise, these chains contribute to a quieter and safer workplace, enhancing overall productivity and employee satisfaction.
Another significant advantage of these Conveyor Chains is their impressive powder recovery rate of 99.4%. This high recovery rate ensures that almost all particulate materials transported by the conveyor system are effectively captured and returned, reducing waste and improving environmental sustainability. This feature is especially beneficial in industries dealing with powdered or granular materials, where loss prevention and cleanliness are paramount.
The Conveyor Chains are also designed to withstand the demanding conditions of curing ovens powered by gas, electricity, or diesel. This compatibility highlights their resilience and adaptability in various industrial processes, including heat treatment and drying applications. Whether used in a gas-fired curing oven, an electrically heated system, or a diesel-powered setup, these chains maintain their structural integrity and performance, ensuring consistent operation without degradation.
In addition to their functional benefits, these Conveyor Chains are constructed from high-quality materials that resist corrosion, abrasion, and mechanical stress. This robust construction extends the service life of the chains, reducing the frequency of maintenance and replacement, and thereby lowering operating costs. The ease of installation and maintenance further enhances their appeal, allowing for quick integration into existing conveyor systems and minimizing downtime.
For industries utilizing Conveyor Stackers, these chains ensure smooth and reliable stacking of materials, preventing jams and ensuring uniform layering. Their precise engineering and compatibility with Chain Mesh Conveyor Belts facilitate seamless material transfer and handling, contributing to streamlined operations and improved throughput.
In summary, the Conveyor Chains are a high-performance solution tailored for various conveyor applications, including Grain Chain Conveyor, Conveyor Stacker, and Chain Mesh Conveyor Belt systems. With a speed capacity of 50 feet per minute, low noise operation, an outstanding powder recovery rate of 99.4%, and compatibility with gas, electricity, and diesel curing ovens, these chains provide unmatched reliability and efficiency. Their durable construction and ease of maintenance make them an indispensable asset in enhancing production workflows and achieving optimal material handling results.
Features:
- Product Name: Conveyor Chains
- Guarantee: 1 year
- Maintenance: Low maintenance required
- Pretreatment: Made with PVC, PP, or SUS material
- Width: 2 inches
- Speed: Operates at 50 feet per minute
- Part of the Conveyor Series for versatile industrial applications
- Compatible with Cylinder Conveyor Chain systems
- Designed for use in Industrial Chain Conveyor setups
Technical Parameters:
| Load Capacity | 5000 Lbs |
| Length | 10 Feet |
| Type | Conveyor Chain |
| Noise Level | Low |
| Booth | PP/PVC |
| Curing Oven | Gas/electricity/diesel |
| Standard | ISO |
| Maintenance | Low |
| Speed | 50 Feet Per Minute |
| Guarantee | 1 year |
Applications:
The MW Conveyor Chains, originating from China, are engineered to deliver superior performance in a variety of industrial applications. Designed with a robust load capacity of 5000 lbs, these conveyor chains are ideal for heavy-duty operations where durability and reliability are paramount. The chains undergo pretreatment using high-quality PVC, PP, and SUS materials, ensuring enhanced resistance to wear, corrosion, and temperature fluctuations. With an operational temperature range of 0 to 300 degrees Fahrenheit, they are well-suited for environments that experience moderate thermal variations.
One of the primary application occasions for MW Conveyor Chains is in conveyor sorting systems. These systems require precise and efficient movement of goods to ensure seamless sorting and distribution. The MW conveyor chains provide smooth and stable transport, reducing downtime and increasing throughput in sorting facilities. Their compatibility as a conveyor accessory allows them to integrate effortlessly with existing conveyor sorting mechanisms, enhancing overall system performance.
Another key scenario where MW Conveyor Chains excel is in chain plate conveyor setups. Chain plate conveyors are widely used in manufacturing and packaging industries to transport heavy or bulky items along production lines. The sturdy construction and 10 feet standard length of MW conveyor chains make them ideal for creating customized conveyor solutions that can handle substantial loads without compromising on speed or reliability. Their pretreatment with durable materials also ensures longevity even under continuous operation.
These conveyor chains are also highly suitable for various other industrial applications, including assembly lines, food processing, and automotive manufacturing, where efficient material handling is critical. The MW brand’s commitment to quality and innovation ensures that their conveyor chains not only meet but exceed industry standards, making them a trusted component in conveyor accessory inventories worldwide.
In summary, MW Conveyor Chains provide a versatile and dependable solution for conveyor sorting systems, chain plate conveyors, and other material handling scenarios. Their high load capacity, robust pretreatment, and adaptability to different temperature ranges make them an essential part of any conveyor system aiming to improve productivity and operational efficiency.
Customization:
MW Conveyor Chains offer exceptional customization services to meet the specific needs of your industrial applications. Manufactured in CHINA and compliant with ISO standards, our chains are designed for durability and high performance in various environments. With a temperature range of 0-300 degrees Fahrenheit, these chains are suitable for a wide array of industrial conveyor belts and conveyors system setups.
Our conveyor chains feature low noise levels, ensuring quieter operation in your chain conveyor systems. The pretreatment options include PVC, PP, and SUS materials, allowing for enhanced resistance and longevity depending on your application requirements. Each chain is available in a standard length of 10 feet, with customization options to fit your precise needs.
Trust MW to provide reliable and efficient conveyor chain solutions tailored to optimize your industrial conveyor belts and conveyors system operations, ensuring smooth and consistent material handling.
Support and Services:
Our Conveyor Chains product is backed by comprehensive technical support and services to ensure optimal performance and longevity. We offer expert consultation to help you select the right chain type and specifications for your specific application. Our technical team provides installation guidance, maintenance tips, and troubleshooting assistance to minimize downtime and enhance efficiency. Additionally, we supply detailed product documentation, including drawings, load ratings, and compatibility charts. For ongoing support, we offer inspection services and replacement parts to keep your conveyor system running smoothly. Trust our dedicated support team to deliver reliable solutions tailored to your operational needs.
Packing and Shipping:
Our Conveyor Chains are carefully packaged to ensure maximum protection during transit. Each chain is wrapped in corrosion-resistant material and securely placed in a sturdy wooden crate or reinforced cardboard box to prevent damage. Packaging is designed to withstand rough handling and environmental factors, ensuring the product arrives in perfect condition.
For shipping, we offer multiple options including air freight, sea freight, and ground transportation, depending on the destination and urgency. All shipments are tracked and insured to provide peace of mind. We work with reliable logistics partners to ensure timely and safe delivery of your Conveyor Chains to your specified location.
FAQ:
Q1: What brand manufactures the Conveyor Chains?
A1: The Conveyor Chains are manufactured by the brand MW.
Q2: Are the Conveyor Chains available with a specific model number?
A2: No, the Conveyor Chains do not have a specific model number.
Q3: Where are the MW Conveyor Chains produced?
A3: The MW Conveyor Chains are made in China.
Q4: What materials are used in the MW Conveyor Chains?
A4: The Conveyor Chains are typically made from high-quality steel to ensure durability and strength in conveying applications.
Q5: Can MW Conveyor Chains be customized to fit specific conveyor systems?
A5: Yes, MW offers customization options to ensure the Conveyor Chains meet the specific requirements of your conveyor system.
Contact Details
Hangzhou Ocean Industry Co.,Ltd
Contact Person: Mrs. Lily Mao
Tel: 008613588811830
Fax: 86-571-88844378
Other Products
-
short pitch / long pitch roller Conveyor chain with High precision
-
Hollow Pin Chain , type C2042HP C2052HP C2062HP C2082HP C2042H-HP C2052H-HP C2062H-HP C2082H-HP
-
Hollow pin chain , type 08BP , 40HP , 50HPSS , 60HP
-
Stainless Steel Straight Run Flat-Top Chain, type LF820-K325 LF820-K350 LF820-K400
-
Stainless Steel Sideflex Flat-top Chain, type 882TAB-K750 , 882TAB-K1000 , 882TAB-K1200
-
Stainless Steel Sideflex Flat-top Chain, type 880TAB-K325 880TAB-K325 882TAB-K500 882TAB-K600